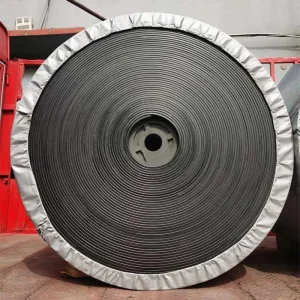
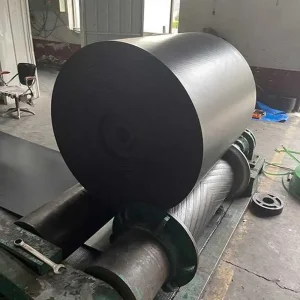
As a leading authority in material handling, Hebei Boao Rubber Technology Co., Ltd. delivers high-performance food-grade belts designed for hygiene, safety, and durability. Our R&D centers leverage 22 years of industry experience to meet stringent FDA/EU food contact regulations.
Strict quality control from raw materials to final vulcanization.
Seamless logistics supporting major food processing hubs worldwide.
Tailored belt specifications for freezing, heating, and high-abrasion zones.
The food grade conveyor industry is shifting towards Anti-Microbial Surfaces and Energy-Efficient Lightweights. As a premier Chinese manufacturer, Boao leads with proprietary vulcanization technology that ensures zero chemical migration, essential for modern food safety compliance. We integrate localized support for global clients, ensuring every belt meets specific regional safety standards.
Yes, our food-grade series undergoes rigorous migration testing to meet global safety benchmarks.
We leverage advanced logistics partnerships to ensure door-to-door delivery with full insurance.
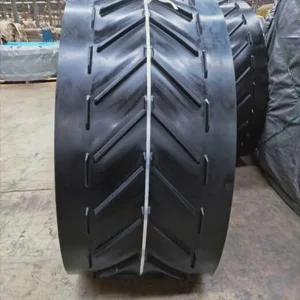
Our factory offers bespoke chevron, herringbone, and custom-width patterns for specific load requirements.
 Boao Rubber